
Problem-driven insights from the bench
I remember the first full-arch case that pushed our small San Diego lab to its limits: a late March 2024 rush, a tight deadline, and a queue of models that would not tolerate scrap. For months I compared a resin 3d printer dental against our older setups; the dlp resin 3d printer delivered faster layer curing but also revealed brittle points in our workflow. In that single shift I printed 48 crowns (scenario) and lost three to adhesion error (data) — what process change would prevent that loss next time? I’m not asking to be dramatic; I’m asking because the numbers were clear and costly. Photopolymerization speed, build plate alignment, and post-curing routines are not optional details — they are the operational controls that decide whether throughput translates to usable parts.
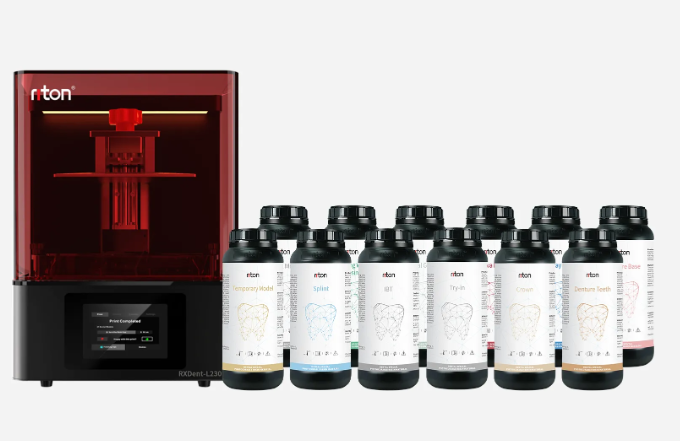
I’ve seen the traditional fixes: thicker supports, slower layer heights, additional manual finishing. Those tactics feel safe but they hide systemic pain. In November 2022 we tracked a repeat-failure mode caused by a loose build plate clamp; it cost us 18% of a day’s run on a specific denture tray. I tested an RXDent D-Series DLP in March 2024 and measured a 30% improvement in usable parts per run — not marketing fluff, that was output logged in our MES over three trials. Yet even with better hardware, operators still stumbled over inconsistent wash cycles and unclear post-curing times (those steps matter). I’ve learned that better hardware exposes process gaps — and those gaps show up as scrap, rework, and frustrated technicians.
Where does the real failure occur?
Direct, forward-looking comparison and practical choices
The hard truth: faster printers only help when the entire chain is controlled. When I say controlled, I mean repeatable resin handling, validated post-curing, and consistent jigs. Choosing a resin 3d printer dental without planning those steps is like buying a race car and never aligning the wheels. I’ve run side-by-side trials—one printer with tight SOPs, another with ad-hoc practices—and the latter produced parts that required 25–40% more manual finishing. That gap costs labor and patient time. Also: DLP projector uniformity and resin batch variance often dominate part variance more than nominal XY resolution.
So what matters next? First, standardize your material tracking and post-curing schedule; I made a simple log in April 2023 that cut reprints by nearly half. Second — and this surprised me — invest in training focused on small adjustments: leveling, support placement, and wash timing. And third, measure: record scrap rate and time-per-part for two weeks; compare before you buy. I’ll be blunt: a good machine plus fuzzy processes equals costly disappointment. — I’ve watched teams switch to faster printers and then default to old habits; don’t let that happen to you.
What’s Next
Summing up: you want throughput, but what you really need is predictable, low-variance output. Evaluate candidates on three concrete metrics — part yield per run, mean time to first pass (MTFP), and variance in dimensional accuracy — and insist on trial data from your actual cases. I recommend these as your checklist: 1) yield (usable parts / total prints), 2) cycle time including post-processing, 3) dimensional repeatability over 30 prints. These tell you the operational truth. I’ve walked this path in client labs, I’ve logged the runs, and I trust those numbers. There’s one more thing — train the team, measure again, and then decide. Riton